


Stainless Steel 304 Laser Cleaning
Laser cleaning removes scale, heat discoloration, and shop residue from 304 stainless tanks, sinks, and fabricated equipment without disturbing the passive chromium oxide layer und...


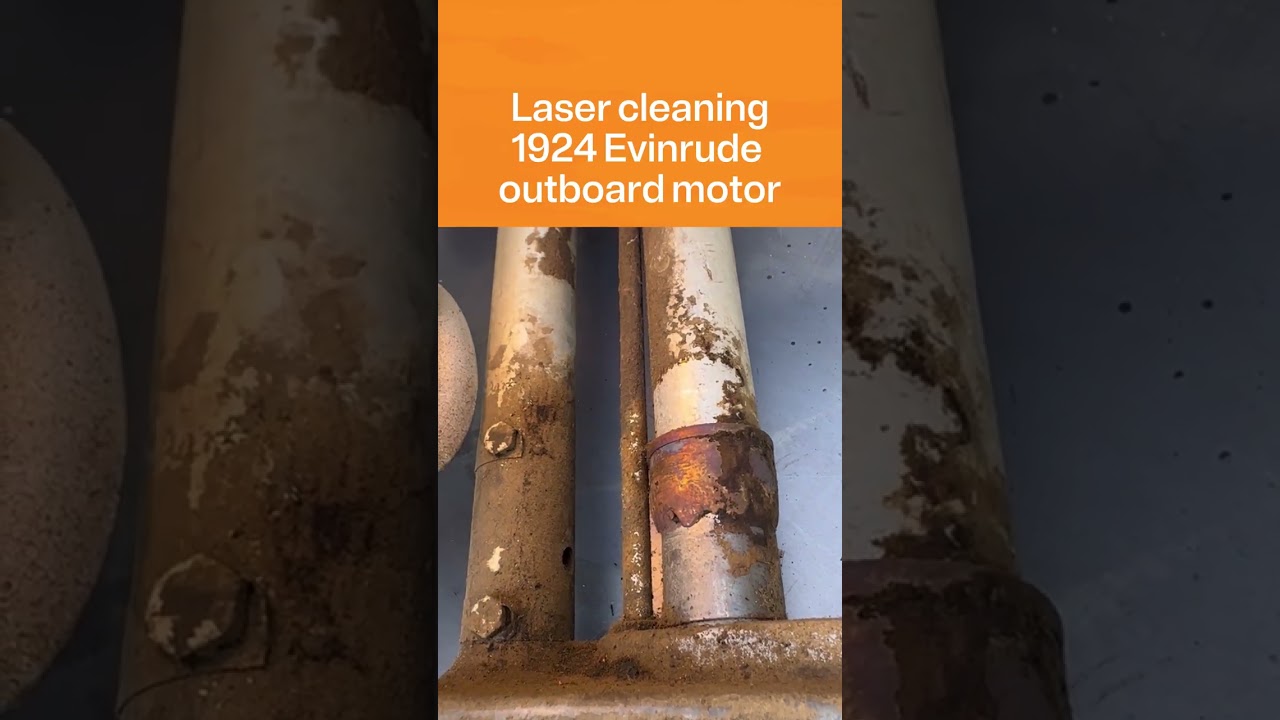
Laser cleaning removes rust, old paint, and corrosion from an antique Evinrude outboard shaft drive down to sound cast iron or bronze without touching the base metal. This rust removal work and paint removal strip the deposits layer by layer, but it will not repair worn seals, straighten a bent shaft, or restore a scored bore. Fit and running clearance still need a mechanical check after cleaning.
Short -mSvxhIuTuI shows pulsed laser clearing rust and old coatings from an antique Evinrude outboard shaft drive while steel and bronze stay in frame.
Laser cleaning removes scale, heat discoloration, and shop residue from 304 stainless tanks, sinks, and fabricated equipment without disturbing the passive chromium oxide layer und...

Laser cleaning removes rust, mill scale, and weld discoloration from steel without media, holding fluence near a 1.5 J/cm² cleaning floor and stopping short of the 4.5 J/cm² mark t...
Atmospheric rust comes off [carbon steel](/materials/steel-laser-cleaning) and [cast iron](/materials/cast-iron-laser-cleaning) under pulsed light as oxide dust, not a solvent wash. What matters is pit depth, whether mill scale sits underneath, and keeping energy below the point that melts thin stock. Extraction has to catch the oxide load, and a heavily pitted plate may still need a mechanical step before the laser.
Dense magnetite scale on [hot-rolled steel](/materials/steel-laser-cleaning) needs more than one careful pulsed pass, unlike a light rust bloom on the same plate. The same laminate can show up on [hot-work tool steel](/materials/tool-steel-laser-cleaning) after forging heat. What matters is naming the film correctly before setting power, keeping extraction live on the heavy oxide dust, and not treating the job like a rust-only wipe. Thin stock can still mark if energy runs high before the laminate is fully gone.
Anneal and service heat grow a bonded oxide scale on [steel](/materials/steel-laser-cleaning), [stainless steel](/materials/stainless-steel-laser-cleaning), titanium, and Inconel that pulsed light separates through thermal expansion mismatch rather than grinding or acid pickling. What matters is each metal's own melt ceiling, chromium-bearing dust on stainless and Inconel, and a coupon-proven setting before the production part. Clearing scale is not the same as restoring corrosion resistance.
Cured paint and powder films leave [steel](/materials/steel-laser-cleaning) and [aluminum](/materials/aluminum-laser-cleaning) hosts once a pulsed beam reaches the pigment's own breakdown point instead of chasing the metal or wood underneath. What matters is naming the pigment chemistry before the pass, capturing lead- or chromate-bearing dust the moment it forms, and proving the exact setting on a labeled coupon rather than trusting one universal recipe. A shop that skips either the chemistry check or the coupon walk risks leftover binder on one host or a scorched surface on the next.
Shop grease and oil sit on [steel](/materials/steel-laser-cleaning) and [aluminum](/materials/aluminum-laser-cleaning) as films that soak into surface roughness, then come off under pulsed light as heat breaks the hydrocarbon apart at the metal. What matters is leftover film that blocks a weld or a coat, smoke from the burned oil, and proving a water-break land on scrap before the production part. A wet degrease line is the other path this job replaces.

Salt air, not the hourly rate, decides a Bay Area rust job. Laser cleaning takes field [rust](/contaminants/iron-oxide-rust-laser-cleaning) off [steel](/materials/steel-laser-clean...

Weld preparation laser cleaning removes rust, mill scale, oil, and drawing compound from a joint face right before the arc or beam strikes, so the fitter is not grinding or wire-br...

A Bay Area body shop stripping failed epoxy or polyurethane before recoat runs into a VOC cap near 50 grams per liter on solvent surface prep and spray-line cleanup, and older meth...
