


Cast Iron Laser Cleaning
Gray and ductile cast iron keep graphite in the matrix. That graphite is supposed to stay there. Rust and foundry scale can come off with a dry laser pass when a copied steel setti...


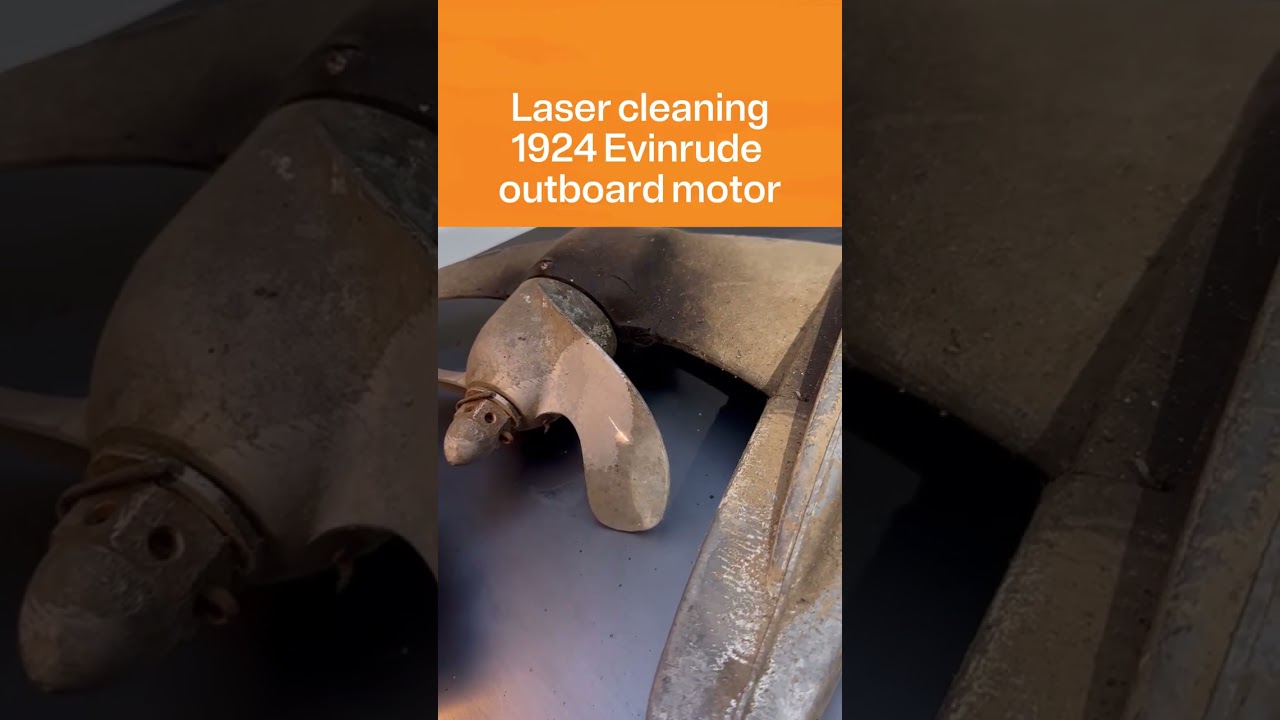
Laser cleaning removes decades of oxidation, old paint, and corrosion from antique Evinrude outboard motor parts without touching the base metal underneath. The method works well on cast aluminum housings, powerheads, and cast iron cylinder blocks, stripping old paint and surface rust layer by layer so casting numbers and original finish stay readable. It won't fill pitting, straighten warped fins, or repair cracked castings; those need machining or welding before any cleaning step. Thin die-cast zinc trim pieces and pot-metal carburetor bodies need lower power and slower passes than the aluminum block, since the same setting that clears rust off cast iron can dull soft alloy edges. Owners restoring a full powerhead usually treat each material separately: aluminum first, then steel fasteners, then the zinc trim, rather than one setting across the whole motor.
Short pxYL0Zdc7iI shows pulsed laser clearing marine corrosion, paint, and oxide from antique Evinrude outboard motor parts across aluminum, bronze, and steel without grit.
Gray and ductile cast iron keep graphite in the matrix. That graphite is supposed to stay there. Rust and foundry scale can come off with a dry laser pass when a copied steel setti...

Nickel in the shop is either solid stock or bar, or a thin plated layer bonded to steel for corrosion resistance. Laser cleaning removes oxide, tarnish, and surface contamination f...

Outdoor sculpture and marine hardware in bronze can lose corrosion and later coatings with a dry laser pass when the grade is known and copper-bearing dust is captured at the head....

Laser cleaning removes worn coating residue, oxidation, and binder smear from titanium carbide surfaces without chemical strippers or abrasive blast media that would round a cuttin...

Zinc shows up as die-cast parts, rolled sheet, and galvanized coatings. A pulsed laser can take native oxide and white rust off the face when energy stays inside a gentle range for...
Anneal and service heat grow a bonded oxide scale on [steel](/materials/steel-laser-cleaning), [stainless steel](/materials/stainless-steel-laser-cleaning), titanium, and Inconel that pulsed light separates through thermal expansion mismatch rather than grinding or acid pickling. What matters is each metal's own melt ceiling, chromium-bearing dust on stainless and Inconel, and a coupon-proven setting before the production part. Clearing scale is not the same as restoring corrosion resistance.
Cured paint and powder films leave [steel](/materials/steel-laser-cleaning) and [aluminum](/materials/aluminum-laser-cleaning) hosts once a pulsed beam reaches the pigment's own breakdown point instead of chasing the metal or wood underneath. What matters is naming the pigment chemistry before the pass, capturing lead- or chromate-bearing dust the moment it forms, and proving the exact setting on a labeled coupon rather than trusting one universal recipe. A shop that skips either the chemistry check or the coupon walk risks leftover binder on one host or a scorched surface on the next.
Workpiece metal that pressure-welds onto a [tool steel](/materials/tool-steel-laser-cleaning) rake or a [carbide](/materials/tungsten-carbide-laser-cleaning) cutting edge comes off under pulsed light so the tool can cut again. What matters is telling the deposit from the tool itself, avoiding a nicked edge, and capturing metal dust as it leaves. Prove the pass on a spare tool first because the deposit and the host can share the same color and the same base metal.
Copper oxide films come off under pulsed light when the job calls for bright [copper](/materials/copper-laser-cleaning) rather than a kept patina. What matters is stopping before the beam cuts into the copper, capturing the oxide fume, and proving the land on scrap because a wanted patina and an unwanted tarnish need different end points.
Black crust and carbon film on [marble](/materials/marble-laser-cleaning) and [limestone](/materials/limestone-laser-cleaning) come off under pulsed light once the soil absorbs far more energy than the pale stone it sits on. What decides the outcome is telling gypsum crust from a thin soot film or a living biofilm, treating sandstone as its own coupon job because its safe margin runs a fraction of marble's, and capturing the crust dust so it does not resettle on the scaffold.

Laser cleaning removes mill scale, oxide layers, and weld residue from fabricated metal parts without abrasive media or chemical strippers. Shops handling [steel](/materials/steel-...
Weld preparation laser cleaning removes rust, mill scale, oil, and drawing compound from a joint face right before the arc or beam strikes, so the fitter is not grinding or wire-br...

Landmark facade work requires a hidden test patch before pulsed laser cleaning touches any visible elevation. The pass removes soot, pollution crust, and graffiti from [brick](/mat...

Precision surface work requires contact-free cleaning because gauge faces, optical flats, and polished tooling scratch under abrasive pads or chemical baths. Pulsed fiber sources r...
